了解储罐为何在真空工况下发生失稳塌陷、真空保护系统可能如何失效,以及工程师在变更真空保护方案前应核实哪些事项。.

A storage tank can collapse under vacuum when pressure inside the tank falls far enough below the pressure outside that the resulting differential exceeds the tank’s actual external-pressure capability. The tank does not need to approach a perfect vacuum before damage becomes possible.
The failure usually develops as a chain rather than as a single bad component. An operating or thermal event first creates an inbreathing demand—the need for gas to enter the tank as internal pressure falls. The protection system must then admit enough gas, through an available and sufficiently unrestricted path, before the pressure differential becomes damaging.
That means a collapsed tank does not automatically prove that the vacuum valve itself failed. A useful investigation separates three questions:
- What created the vacuum demand?
- Why did the protection system fail to control it?
- Why could the tank structure not tolerate the resulting pressure differential?
Those questions are deliberately separate. The first is a process-duty question, the second is a protection-system question, and the third is a tank-integrity question. Treating them as one problem is how a team can replace a vent without correcting the event that created the vacuum, or blame a device that was never sized for the actual duty.
Why Can Vacuum Make a Storage Tank Collapse?
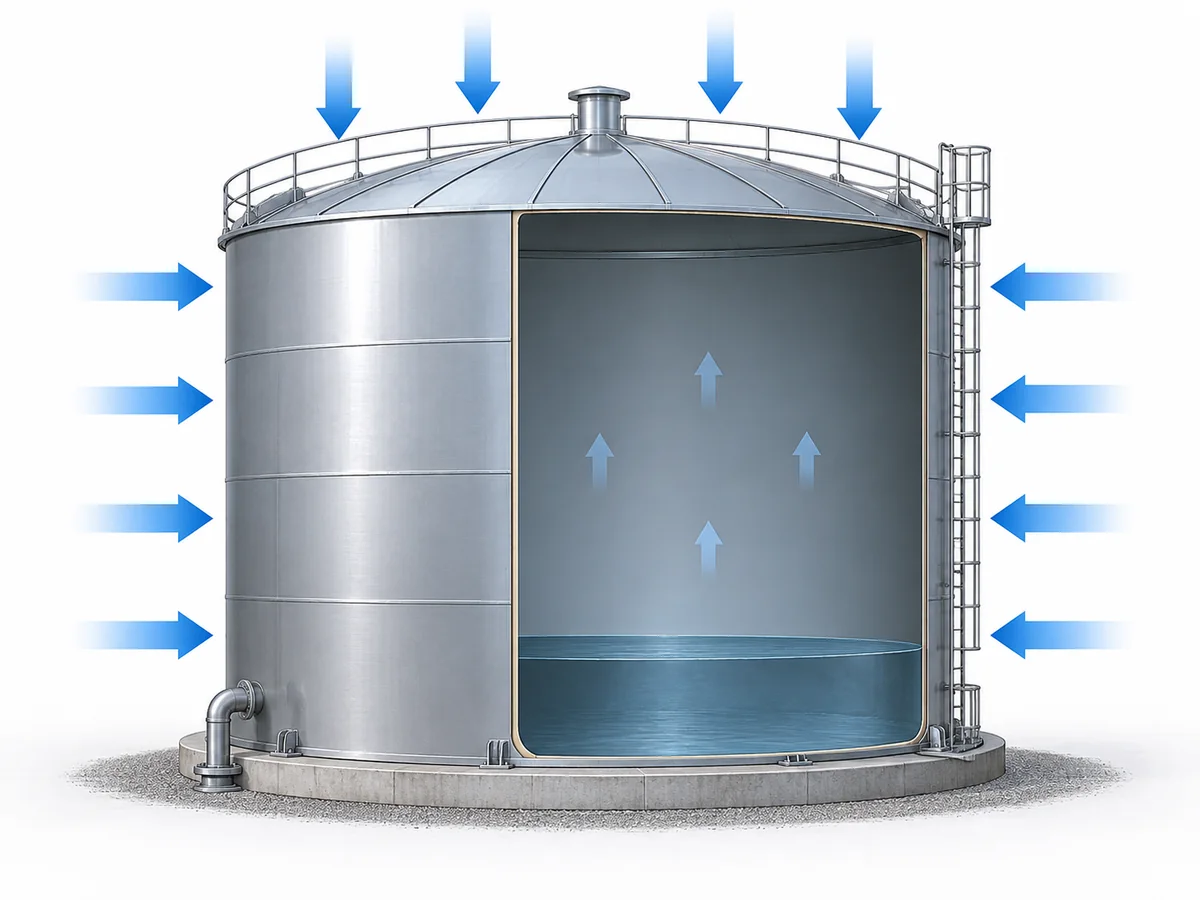
Vacuum collapse is fundamentally an external-pressure problem.
When pressure inside a storage tank falls below the pressure acting outside the tank, the shell and roof must resist the resulting inward pressure differential. If that differential exceeds the actual tank’s structural capability, inward deformation or buckling can occur.
AIChE/CCPS vacuum-hazard guidance warns that equipment rated for internal pressure may not be rated for vacuum. Peer-reviewed storage-tank research likewise treats internal vacuum as external-pressure loading on thin-walled tanks, with buckling sensitivity affected by tank geometry and condition. The practical implication is that a pressure rating cannot be used as a substitute for a documented vacuum or external-pressure capability.
Describing this simply as “vacuum sucking the tank inward” hides the engineering issue. The useful relationship is:
external pressure − internal pressure = pressure differential acting across the tank boundary
The tank must remain structurally stable under that differential.
Thin-walled storage tanks can be particularly sensitive to external-pressure loading because buckling resistance depends on more than the material’s basic strength. Tank geometry, shell thickness, structural details, fabrication imperfections, corrosion, thinning and existing damage can all influence the actual resistance to inward buckling. A 2016 peer-reviewed study of ground-based steel tanks under internal vacuum found that corrosion can materially change buckling strength and failure mode; that is useful evidence for the mechanism, but not a universal collapse threshold.
For that reason, there is no defensible universal vacuum value at which every storage tank will collapse. A 2026 open-access study of a food-storage-tank implosion demonstrated how steam condensation, tank geometry and structural modeling can be combined for one documented incident, while also making clear that the model depended on that tank’s geometry and operating history. The case is evidence that condensation-driven vacuum can be severe; it is not a value to copy into another tank’s design basis.
A tank designed to operate with some positive internal pressure also should not be assumed to have an equal vacuum capability. Internal-pressure resistance and external-pressure stability are different engineering questions.
For a real installation, the meaningful comparison is therefore:
What pressure differential occurred, and how does it compare with the documented vacuum or external-pressure capability of this specific tank?
If that design basis is unknown, the missing information cannot safely be replaced with a generic “safe vacuum” number. Retrieve the tank datasheet, design drawings or applicable engineering calculation, and separately assess whether corrosion, deformation or modification may have changed the as-installed condition.
Engineering evidence: Chemical Engineering & Technology, 2026, documented food-storage-tank implosion study.
What Operating Events Create Dangerous Vacuum in a Storage Tank?
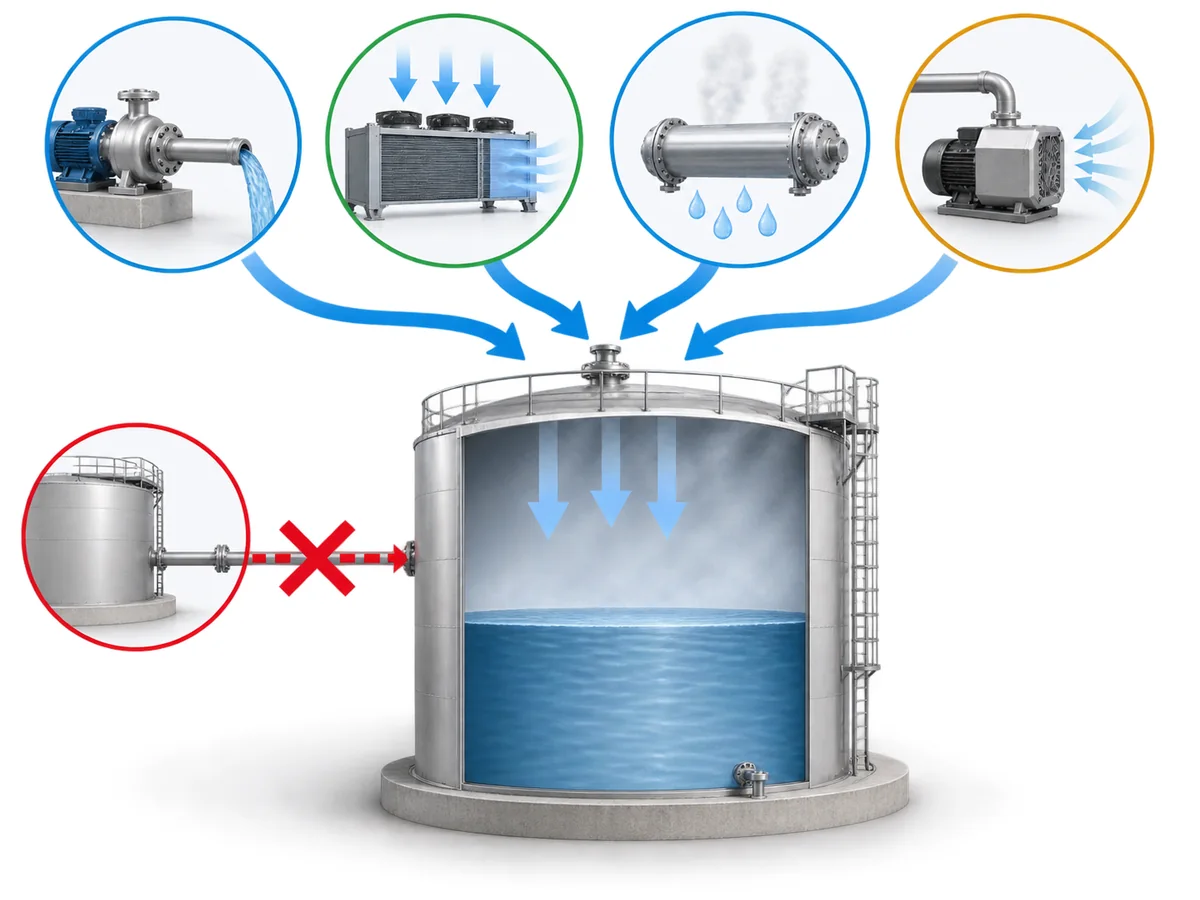
Before inspecting the vacuum valve, identify what was actually driving the tank pressure downward.
Different events produce different inbreathing demands. Treating all of them as the same “vacuum problem” makes it easier to size, troubleshoot or replace the wrong part of the protection system. Related vacuum mechanisms across other equipment are covered separately in ZOBAI’s vacuum service application content.
| Operating event | Why tank pressure can fall | What should be verified |
|---|---|---|
| Liquid withdrawal or pump-out | Removing liquid increases vapor-space volume. Gas must enter fast enough to replace that volume. | Actual withdrawal rate, simultaneous withdrawals if relevant, and available inbreathing path |
| Cooling of the vapor space | Cooling can contract the gas or vapor and reduce internal pressure. | Temperature history, vapor-space condition, weather or process cooling, and operating state |
| Steam or condensable-vapor cooling | Condensation converts vapor to liquid and can rapidly reduce vapor-phase inventory. | Whether relevant condensable vapor was present, whether the tank was isolated, and how cooling occurred |
| Applied vacuum source | A vacuum pump, eductor or connected process can actively remove gas. | Vacuum source, controls, isolation logic, operating sequence and make-up path |
| Combined events | Withdrawal, cooling, condensation or other mechanisms may act together. | Full process timeline rather than one isolated parameter |
Liquid withdrawal creates an inbreathing requirement
When product is pumped out, the vapor space gets larger. Replacement gas has to enter the tank as that volume increases.
If the incoming gas flow through the protection system cannot keep pace with the actual withdrawal condition, internal pressure can continue falling. For applicable U.S. flammable-liquid tanks, OSHA 29 CFR 1910.106 explicitly addresses normal venting for vacuum or pressure caused by filling, emptying and atmospheric temperature changes, and it requires simultaneous flows to be considered where simultaneous filling or withdrawal can occur. That OSHA rule is jurisdiction- and service-specific; it is not a universal global design rule.
That does not mean every pump-out operation is dangerous. The important comparison is between the actual inbreathing demand 以及 available installed capacity to admit replacement gas.
Illustrative engineering scenario — correct opening point, insufficient duty capacity: A tank’s vacuum vent begins to open at the intended setting, but a later process change increases the maximum pump-out rate while the venting basis is left unchanged. The device can be mechanically healthy and still fail to hold tank pressure above the design vacuum because the required inbreathing flow now exceeds the available installed flow. The prevention step is to re-check the venting basis whenever transfer rates or simultaneous withdrawals change, not merely to confirm the set point.
Cooling can create vacuum without pump-out
Tank pressure may also fall while the liquid level is unchanged.
Cooling of the vapor space can reduce gas or vapor pressure. Where steam or another condensable vapor is present, condensation can reduce vapor-phase inventory much more rapidly.
AIChE/CCPS process-safety guidance identifies inadequate venting during draining and cooling, steam condensation, and externally imposed vacuum sources as credible vacuum mechanisms. These mechanisms should still be applied only where the actual process conditions support them.
Documented engineering example — steam-out followed by cooling: AIChE/CCPS describes steam-out as a vacuum hazard because steam can condense rapidly if the equipment is not adequately vented. The 2026 peer-reviewed food-tank study linked a documented implosion to cooling and steam condensation after cleaning. The lesson is not to copy that tank’s pressure history; it is to treat steam-out, isolation status and cooldown as a distinct vacuum scenario that may require a different inbreathing basis from routine pump-out.
A strong external vacuum source is a separate scenario
A connected vacuum pump, eductor or other system capable of actively removing gas can create a different duty from ordinary tank breathing.
The protection basis must reflect the actual scenario rather than assuming that normal thermal breathing or routine pump-out defines the worst credible vacuum demand. If the vacuum source is capable of drawing pressure down faster than the make-up or relief path can respond, the correct engineering question is whether the tank is designed for that vacuum or whether the system provides a positively available means of limiting it.
A blocked vent is usually not the whole explanation
A blocked, covered or fouled vent may explain why pressure could not equalize, but an investigation should still determine what was causing pressure to fall.
Pump-out / cooling / condensation → vacuum demand develops → vent or make-up path unavailable or inadequate → internal pressure continues falling
AIChE/CCPS’s February 2007 Process Safety Beacon on collapsed tanks documents cases involving intended vent paths that were covered or plugged. The engineering lesson is broader than “keep the vent clean”: the pressure-driving event and the failed protection path need to be identified separately.
Why Can Vacuum Protection Fail Even When a Vent or Valve Is Installed?
Seeing a breather valve, pressure-vacuum vent, vacuum-relief valve or blanketing system on a storage tank does 不 establish that the tank is adequately protected.
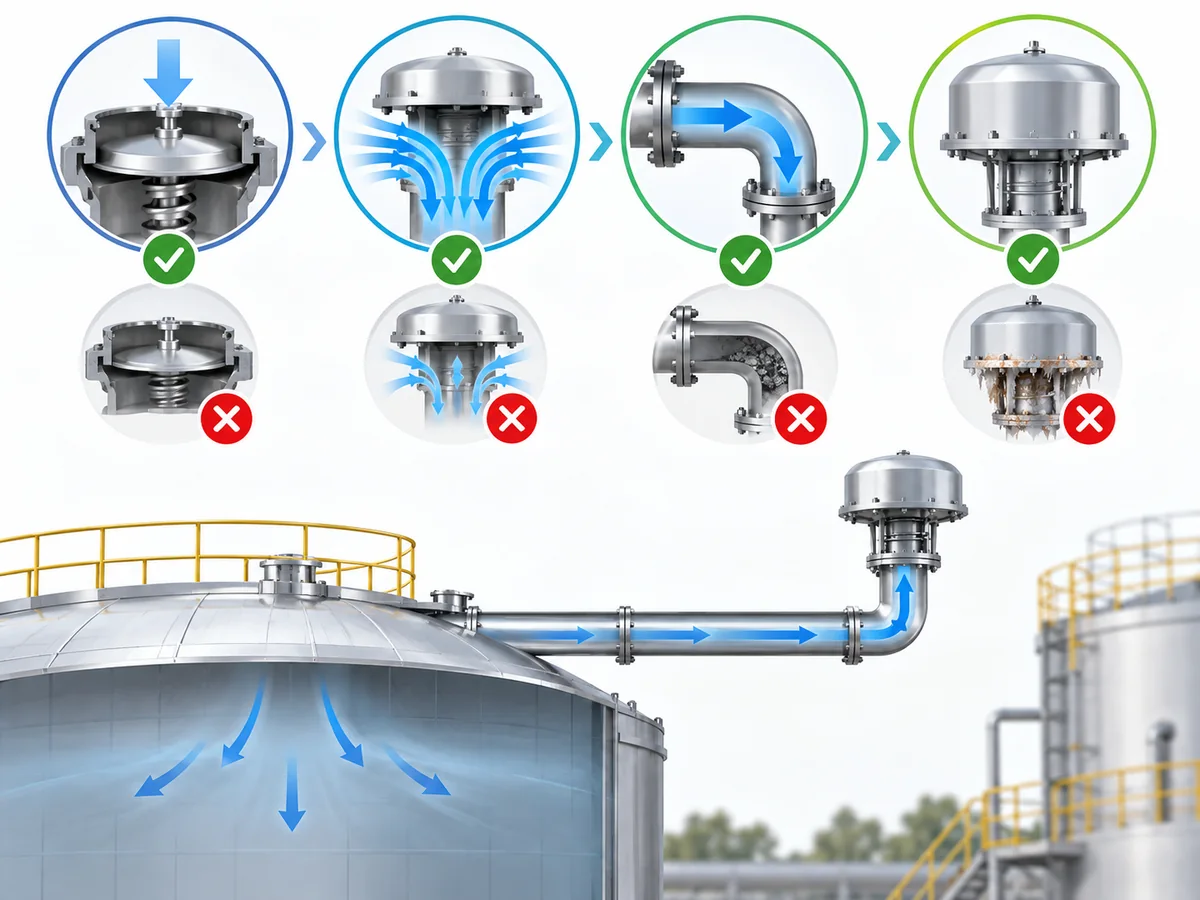
Effective vacuum protection requires several different conditions to be satisfied at the same time. A device can have the intended opening setting yet still be inadequate because the required inbreathing capacity was underestimated, the installed path adds more resistance than the sizing basis assumed, the path is unavailable, or the process has changed.
| Protection layer | What can fail | What must be established |
|---|---|---|
| Design basis | The actual pump-out, thermal or abnormal vacuum case was not included in the original basis. | Which scenarios the protection system was designed to handle |
| Opening condition | The device response is not adequately coordinated with the tank’s allowable vacuum. | Actual setting and documented tank limit |
| Flow capacity | The device opens but cannot admit gas fast enough for the actual duty. | Required inbreathing rate versus documented flow performance |
| Installed flow path | Piping, screens, flame arresters or other components introduce restriction. | Complete installed configuration and pressure losses relevant to the duty |
| Availability | The path is blocked, covered, isolated, fouled or otherwise unavailable. | Physical configuration during the event |
| Device condition | The installed unit does not function as intended. | Inspection, maintenance or test evidence |
The most important distinction is:
Correct setting ≠ adequate capacity ≠ adequate installed flow path ≠ guaranteed availability.
This separation is also reflected in tank-venting guidance. Manufacturer vent-sizing guidance treats tank design vacuum, vent set point, required flow and vent flow capability as separate inputs. The source is useful for device/application mechanics; the applicable code basis and final duty still have to come from the project.
Opening at the right vacuum is not enough
A vacuum-relief device can begin opening at its intended condition and still fail to protect the tank if the required inward gas flow is greater than the flow the system can actually deliver.
Opening condition answers:
When does the device begin responding?
Capacity answers a different question:
Can enough gas pass through the protection system to control the pressure drop?
Those cannot be treated as interchangeable specifications. A capacity check must use the credible inbreathing case and the documented performance basis for the device or system; connection size alone does not establish capacity.
Nominal valve size is not installed-system capacity
Device performance is established under defined conditions. The installed protection path may contain additional piping, screens, weather protection, flame arresters, nozzles or other components.
Those components can add resistance. The engineering comparison is therefore between required inward flow 和 available flow through the complete installed path at an acceptable tank pressure, not merely between two flange sizes.
Required inward flow vs. available flow through the complete installed path
Illustrative engineering scenario — accessory added after the original sizing: A tank vent was originally selected against the transfer duty with a short, low-restriction path. A flame arrester or additional vent-line hardware is later installed, or an existing element becomes fouled. The valve’s own published flow capability has not changed, but the pressure drop of the installed path has. The correct action is to review the complete path against the tank’s allowable vacuum and required inbreathing flow rather than assuming the existing nominal valve size remains adequate.
A protection path must also be physically available
A correctly selected device cannot perform its intended function if replacement gas cannot reach the tank.
During a vacuum-collapse investigation, the physical path therefore matters just as much as the device nameplate:
- Was anything covering the vent?
- Was there fouling, deposits, debris, icing or another obstruction relevant to the service?
- Could an isolation point interrupt the flow path?
- Had piping, flame-protection hardware or other accessories been modified?
- Was the actual installed arrangement the same as the design basis?
These are checks, not predetermined diagnoses. A collapsed tank does not prove that the moving parts of the vacuum valve stuck; it may instead show that the required flow never reached the device or the tank through the assumed path.
Blanketing is not automatically a substitute for vacuum relief
Gas blanketing can influence tank pressure, but the existence of a nitrogen or other blanketing system does not by itself prove that every credible inbreathing demand is protected.
The available make-up capacity, supply pressure, pressure-control arrangement and interaction with other protection layers have to be understood for the actual installation. Current manufacturer tank-management architectures commonly show blanketing, pressure/vacuum relief, flame protection and emergency venting as separate layers rather than interchangeable functions.
Illustrative engineering scenario — blanketing credited beyond its proven capacity: A blanketing regulator maintains slight positive pressure during ordinary breathing, so the design team assumes it also covers the maximum pump-out case. If the credible withdrawal rate exceeds the regulator and supply system’s demonstrated make-up capacity, tank pressure can still fall toward the vacuum-relief setting. The prevention is to define what duty is assigned to blanketing, what duty is assigned to independent vacuum relief, and whether both remain available during the same event.
There is also another process boundary: in some inerted or flammable services, unrestricted admission of atmospheric air may create a separate hazard. AIChE/CCPS specifically notes that vacuum can draw air into flammable equipment. Vacuum protection therefore cannot always be simplified to “open the tank to more air.”
The correct protection strategy depends on the process as well as the tank.
For device-level information after the duty has been defined, see ZOBAI’s vacuum safety valves page. This article does not use that product page to infer suitability for any specific tank.
How Should You Investigate a Vacuum Collapse or Near Miss?
A deformed tank is evidence that something went wrong, but it is not a root-cause diagnosis.
A useful investigation moves from the operating event through the complete protection system instead of beginning with the assumption that one valve failed.
The sequence below is an engineering investigation framework for organizing evidence. It is not a universal regulatory checklist, a substitute for a formal incident investigation, or a remote root-cause determination.
1. Reconstruct the actual operating event
Establish what was happening immediately before and during the pressure excursion.
Relevant evidence may include:
- pump or transfer status and actual withdrawal rate;
- liquid level changes;
- temperature history;
- cleaning or steaming sequence;
- isolation sequence;
- vacuum-system operation;
- blanketing-system behavior and gas-supply availability;
- alarms and process trends;
- maintenance or modification work that could have changed the vent path.
The objective is to rebuild the sequence from recorded evidence rather than from assumptions formed after the tank was damaged.
2. Identify what drove pressure downward
Determine which physical mechanism created the vacuum demand.
Was liquid being withdrawn? Did the vapor space cool? Was steam or another condensable vapor present? Was the tank connected to an active vacuum source?
More than one mechanism may have contributed. A blocked vent should not be used as a substitute for this step: the blockage may explain why the tank could not breathe, but the pressure-driving event still has to be identified.
This question should be answered before the vent is declared the cause.
3. Establish the tank’s documented pressure and vacuum basis
Retrieve the actual tank design information.
The relevant question is not whether the tank normally operates near atmospheric pressure. It is what external-pressure or vacuum condition the tank was designed to withstand, and whether later modifications or deterioration may have changed the as-built condition.
Do not infer this value from:
- tank diameter alone;
- the operating pressure;
- another similar-looking tank;
- an unrelated storage-tank standard;
- the installed vacuum valve setting.
4. Identify the protection that was intended to respond
Determine what was supposed to limit the vacuum:
- a vacuum pallet in a P/V vent;
- a dedicated vacuum-relief device;
- a gas make-up or blanketing arrangement;
- another engineered vent path;
- or a combination of protection layers.
Without knowing the intended architecture, it is impossible to establish whether the system actually performed as designed.
5. Trace the full inbreathing path
Follow the route replacement gas was expected to take into the tank.
Check the actual installation, including relevant:
- vent piping;
- nozzles;
- screens;
- flame arresters;
- isolation points;
- covers or weather protection;
- other accessories.
A valve can be serviceable while the overall path remains unavailable or too restrictive.
6. Inspect the protection device rather than inferring its condition
Verify its configuration, set condition and physical condition from appropriate documentation, inspection and, where applicable, testing.
Do not work backwards from the collapsed tank and treat valve malfunction as already proven.
Device failure is one possible explanation. It is not the only one. If the device is dismantled or serviced as part of the investigation, preserve the relevant as-found observations and records so that maintenance activity does not erase evidence needed to explain the event.
API’s current standards plan lists RP 575, Inspection Practices for Atmospheric and Low-Pressure Storage Tanks, 以及 RP 576, Inspection of Pressure-relieving Devices as current API documents, with recent 2025–2026 addenda. Use the editions required by the project or jurisdiction; this article does not prescribe a fixed inspection interval.
7. Compare the actual duty with installed capability
Once the vacuum-generating scenario is understood, compare that demand with the documented performance of the complete protection path.
This is where three values that are often confused have to remain separate:
- device opening condition;
- required inbreathing flow;
- available installed flow capability.
A satisfactory answer to one does not automatically answer the others. If the vent has a documented flow curve, the relevant comparison is the flow available before the tank’s allowable vacuum is exceeded under the actual installed conditions.
8. Check whether operating conditions changed
A system originally designed for one duty may become inadequate after a change in:
- pump or transfer rate;
- operating procedure;
- cleaning method;
- tank service or stored fluid;
- blanketing arrangement or gas supply;
- piping;
- vent accessories.
The investigation should compare current operating conditions with the basis used when the protection was originally specified. A change in process duty can invalidate a once-adequate venting basis even when the valve itself has not changed.
9. Review tank condition as a separate factor
Vent performance is not the only variable.
Corrosion, thinning, previous deformation or other structural deterioration can affect buckling resistance. Structural condition should therefore be investigated separately rather than inferred from the valve condition.
10. Escalate structural and restart decisions appropriately
If the tank has already deformed, neither the condition of the vent nor a replacement valve establishes that the tank remains fit for service.
Remaining structural capacity, repair requirements and return-to-service decisions require appropriate inspection and engineering evaluation under the applicable tank-integrity framework.
A technical article can help organize the investigation. It cannot remotely certify the integrity of a damaged tank.
What Must Be Verified Before Changing or Specifying Vacuum Protection?
A replacement vacuum valve should not be chosen simply because it has the same connection size as the old one.
Before specifying new protection, first define:
- the tank;
- the vacuum-generating duty;
- the allowable pressure boundary;
- the complete installed flow path.
Only then does device selection become meaningful.
Information the tank owner or engineer should establish
A useful engineering package includes the information relevant to the actual service, such as:
- tank type, construction and service;
- documented design pressure and design vacuum or allowable external-pressure basis;
- stored liquid and relevant vapor behavior;
- 正常工作压力;;
- maximum credible liquid withdrawal or transfer rate, including simultaneous cases where applicable;
- cooling or condensation case, where applicable;
- any externally imposed vacuum source;
- blanketing or gas make-up arrangement and available supply capacity;
- existing pressure/vacuum protection and its documented setting/capacity information;
- installed piping, flame arresters, screens and other relevant accessories;
- applicable project standard, jurisdiction and required edition.
Not every tank needs every scenario. The purpose is to define the cases that are credible for this installation, then establish which case governs the inbreathing requirement.
The protection-system review should then verify
The engineering or supplier review can evaluate:
- suitability of the proposed protection architecture for the defined service;
- coordination between device opening condition and tank allowable vacuum;
- documented flow performance against the required inbreathing duty;
- impact of installed restrictions and accessories;
- material and process compatibility where relevant;
- interaction between blanketing and independent protection layers;
- whether atmospheric air admission is acceptable for the process;
- required inspection, test and project documentation.
Illustrative procurement failure — selecting by flange size: A replacement vent is ordered with the same nozzle connection as the removed unit, but the old rating basis, actual inbreathing duty and installed accessory pressure loss are not checked. The new device may physically fit and still be the wrong protection. A defensible RFQ therefore starts with the tank design vacuum, governing inbreathing scenario and required capacity—not the connection size.
Treat standards as engineering frameworks, not generic labels
API’s current standards plan lists API Standard 2000, Venting Atmospheric and Low-Pressure Storage Tanks, 8th Edition. ISO 28300:2008 remains the published current ISO edition, while ISO shows a second edition under development. Those references address tank venting, but the project must still confirm the applicable scope, edition and contractual or regulatory basis.
ISO 28300:2008 is written for petroleum and petroleum-product storage tanks and states that application to other liquids requires sound engineering analysis and judgment. It also excludes external floating-roof tanks. That scope matters: citing the standard name is not the same as proving that every storage tank on every service falls within it.
U.S. regulatory requirements are also jurisdiction-specific. OSHA 29 CFR 1910.106 requires adequate normal venting for applicable flammable-liquid storage tanks so filling, emptying and atmospheric temperature changes do not create damaging pressure or vacuum. Its incorporated API Standard 2000 reference is the 1968 edition, so it should not be described as if OSHA automatically incorporates the current API edition.
The same discipline applies when an old datasheet or facility specification cites a legacy standard: establish the actual project basis before converting a historical reference into a current compliance claim.
For the wider pressure, vacuum and emergency protection architecture around tanks, see ZOBAI’s storage-tank venting and protection 应用页面。.
Specify the duty before specifying the valve
The most useful RFQ is not simply, “Please quote a vacuum valve for this flange size.”
It begins with enough information to answer:
What vacuum condition must be controlled, how much inward flow is required, what limit must the tank stay above, and what restrictions exist between the gas source and the tank?
Connection size, nominal pressure or a photograph of the old vent cannot answer those questions. A supplier can only verify capacity, setting and construction against the duty that the owner or engineer actually defines.
Once the duty and system boundary are known, a replacement device or revised protection strategy can be evaluated against the actual tank instead of against assumptions.
Frequently Asked Questions About Storage Tank Vacuum Collapse
What causes a storage tank to collapse under vacuum?
A tank can buckle when internal pressure falls below external pressure far enough that the resulting pressure differential exceeds the tank’s actual external-pressure capability. The pressure drop may be driven by pump-out, cooling, condensation or an applied vacuum source, while inadequate or unavailable inbreathing allows the differential to grow.
Can a storage tank collapse even if a vacuum relief valve is installed?
Yes. Device presence does not prove adequate protection. The opening condition, required inbreathing capacity, installed-path pressure loss, availability of the flow path and actual device condition all have to be compatible with the tank’s allowable vacuum and credible operating cases.
Is a blocked vent enough to explain a tank implosion?
Not by itself. A blocked vent can prevent pressure equalization, but the investigation still needs to identify what was driving pressure downward—such as liquid withdrawal, cooling, condensation or an active vacuum source. The demand event and the failed breathing path are separate parts of the failure chain.
Does nitrogen blanketing replace a vacuum relief valve?
Not automatically. Blanketing can supply make-up gas and control tank pressure, but its capacity and availability must be proven for the assigned duty. Many tank-protection arrangements use blanketing together with pressure/vacuum relief rather than treating them as interchangeable functions.
Why is vent capacity more important than matching the old connection size?
Connection size only describes a physical interface. Protection depends on the gas flow that the complete installed path can pass before the tank’s allowable vacuum is exceeded. A same-size replacement can therefore be inadequate if the process duty, setting, flow curve or system resistance differs from the original basis.
What should be checked before a deformed tank is returned to service?
A replacement vent alone does not establish fitness for service. The event should be investigated, the tank’s design basis and structural condition should be reviewed, and appropriate inspection and engineering evaluation should determine repair and return-to-service requirements under the applicable tank-integrity framework.